Chemistry before the pour
Spectrometer and CE analysis confirm carbon, silicon, magnesium and residuals before metal is tapped.
Spheroidal graphite (ductile) iron castings from 0.5 to 200 kg, made to IS 1865 or your specification in our Delhi NCR foundry, with nodularity checked on every heat.
SG iron, also called ductile iron or nodular cast iron, gets its toughness from graphite that forms as round nodules instead of flakes. That gives it high tensile strength, real elongation and good impact resistance, which can replace fabricated steel and forgings in many load-bearing parts at lower cost.
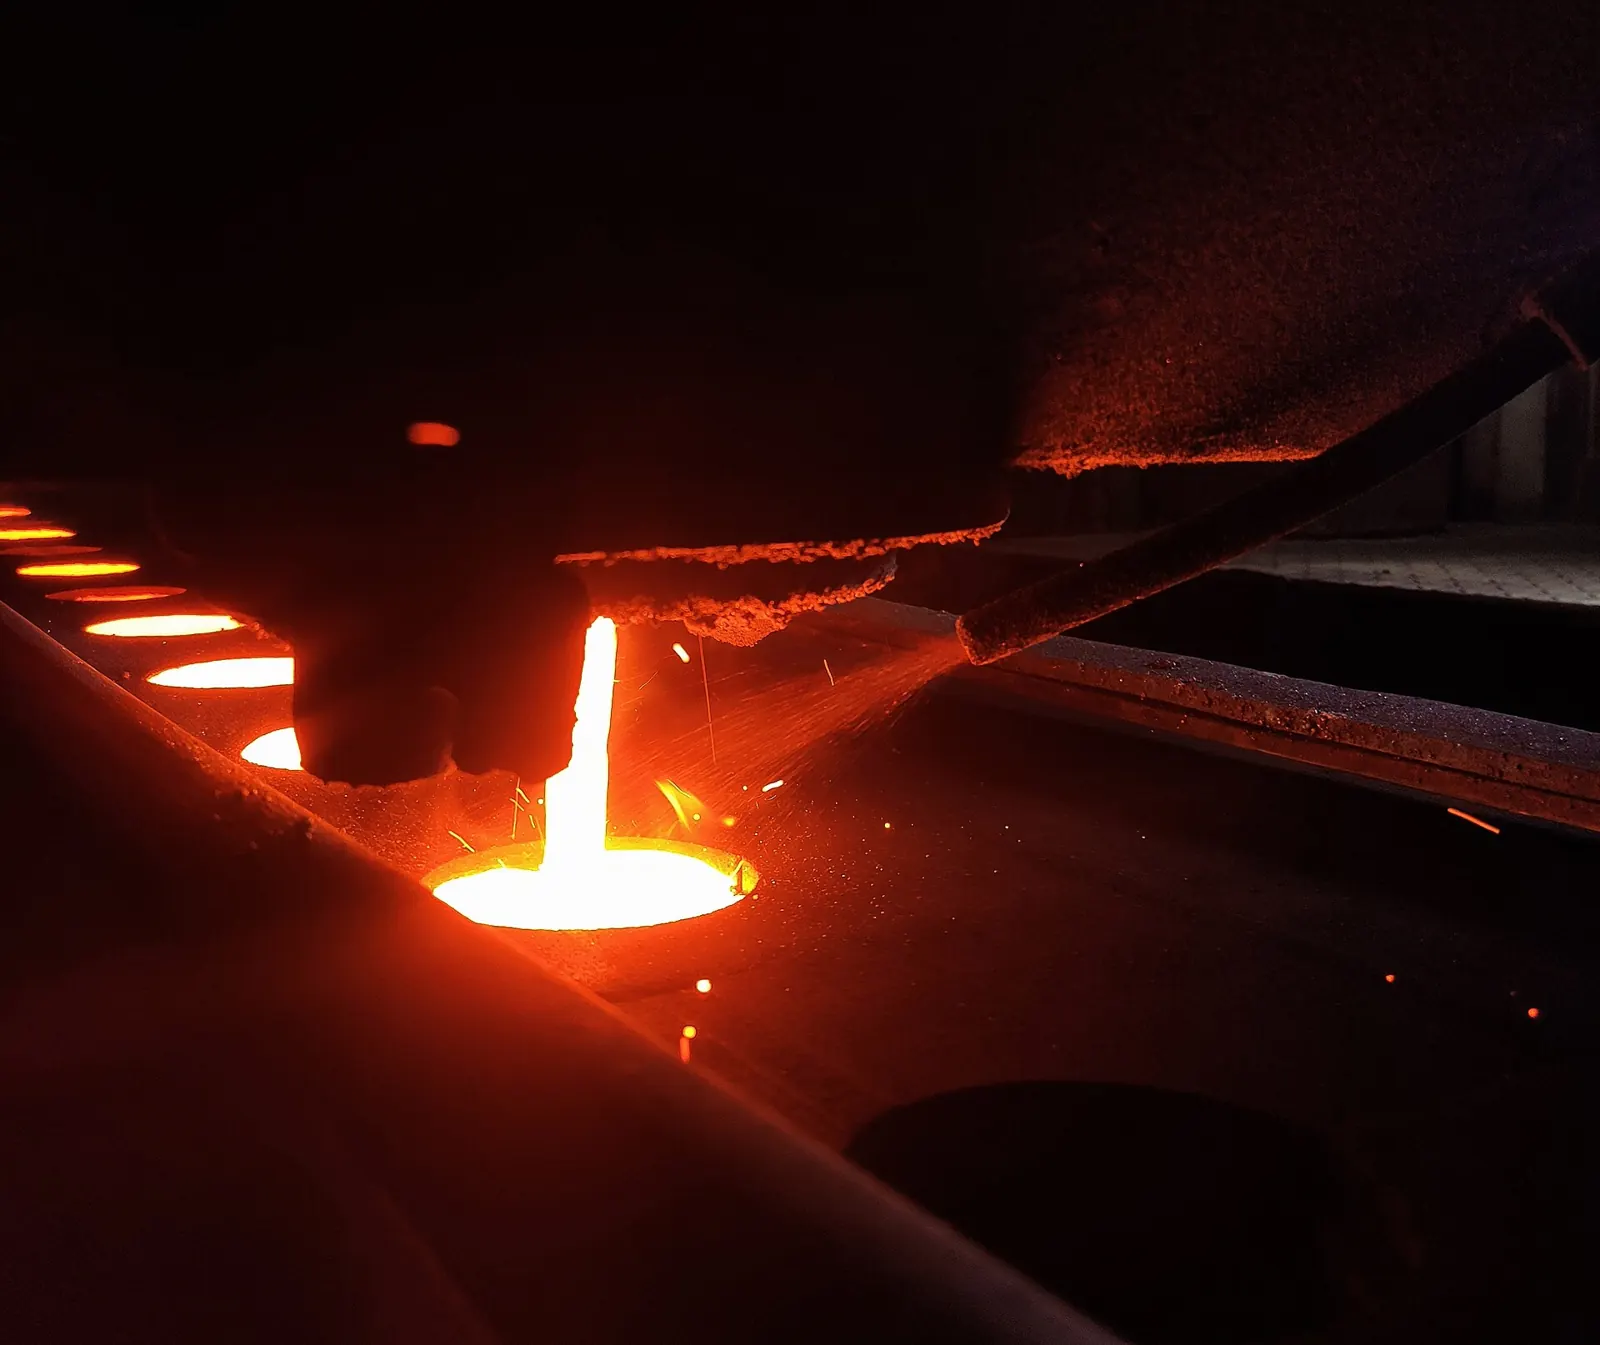
We melt SG iron in an Inductotherm double-crucible induction furnace, treat and inoculate it under controlled practice, and pour it on high-pressure and APRA 300 moulding lines. Every heat is checked for chemistry and microstructure before castings are released.
| Grade (IS 1865) | Tensile min (MPa) | 0.2% proof min (MPa) | Elongation min (%) | Typical HB | Matrix |
|---|---|---|---|---|---|
| SG 400/15 | 400 | 250 | 15 | 130–180 | Ferritic |
| SG 450/10 | 450 | 310 | 10 | 160–210 | Ferritic |
| SG 500/7 | 500 | 320 | 7 | 170–230 | Ferritic-pearlitic |
| SG 600/3 | 600 | 370 | 3 | 190–270 | Pearlitic-ferritic |
Typical values on separately cast test bars. Final properties depend on section thickness and the agreed specification.
Spectrometer and CE analysis confirm carbon, silicon, magnesium and residuals before metal is tapped.
Micro image analysis measures nodularity, nodule count and ferrite / pearlite ratio against your grade.
Brinell hardness is recorded heat-wise, so every dispatch lot traces back to its heat.
Can't find your answer? Call +91 88600 73338 or email sales@ferrotechalloys.com.
We regularly cast SG 400/15, SG 450/10, SG 500/7 and SG 600/3 to IS 1865, equivalent to EN-GJS-400-15, 450-10, 500-7 and 600-3. Other grades and customer specifications can be discussed with your enquiry.
We produce SG iron castings from 0.5 kg to 200 kg per piece. Moulding boxes are 650 × 750 mm on the high pressure line and 550 × 600 mm on the APRA 300 line.
Every heat is sampled and examined on our micro image analyser, which measures nodularity and nodule count. Chemistry is confirmed beforehand by spectrometer and CE analyser.
Yes. Our in-house machine shop has 4 CNC turning centres, 2 VMCs, 6 SPMs and drilling machines, plus an automated powder coating plant, so castings can be supplied as-cast, machined, or machined and coated.
Chemistry, microstructure and hardness results are recorded heat-wise under our ISO 9001 system and can be supplied with dispatches on request.
Share a drawing, grade and annual quantity. Our engineering team reviews every enquiry for methoding, tooling and machining, then comes back with a detailed quotation.